Dust fan balance in MDF sawing and cutting workshops is the process of correcting the unbalanced mass distribution of the centrifugal suction impeller through dynamic balance in the working place, which neutralizes the vibration fluctuations and reduces the acoustic noise caused by resonance by more than 70% immediately. Accumulation of fine dust, MDF resin glue and asymmetric erosion of the blades make the axial mass of the propeller out of symmetry and make the shaft vibrate. Fixing this imbalance with the methods of vibration analysis and specialized balancing weight is the only scientific method to stop continuous screaming and decrease the depreciation of bearings without replacing the entire duct system.
The root of the unpleasant sound of wooden vacuum cleaners; Mass imbalance or acoustic resonance?
In field visits to wooden products production lines and PVC and MDF cutting service workshops, most of the technicians think that the origin of the deafening howling of vacuum cleaners is simply the passage of air inside the galvanized pipes. In practice, it has been observed that more than 80% of the low-frequency and impact noise of these facilities is caused by the radial slip caused by the imbalance of the suction impeller.
The round particles of chipboard and medium density fiber (MDF) carry dry chemical resins. These particles stick to the corners of the radial or backward blades during high speed suction. As soon as a piece of this compressed mass is torn off due to the impact of a piece of wood, the symmetry of the center of mass and the center of rotation of the propeller are disturbed. The centrifugal force vector caused by this mass asymmetry is directly coupled to the shaft, pulley and belt and finally the bearing seat. The result of such a phenomenon is the emergence of rotational vibration with the frequency of the engine revolution, which turns the entire body of the spiral plate into a large diaphragm speaker.
Consequences of unbalanced suction performance beyond noise pollution
The continued operation of a vibrating centrifugal fan in an industrial environment is not only a threat to the hearing of cutting station operators; It starts a chain of heavy financial damages.
Fast wear of bearings and shaft breakage
The dynamic imbalance force has a direct relationship with the square of the rotational speed. This means that with the doubling of the impeller, the vibration load on the bearing balls and rollers is quadrupled. In this condition, the oil or grease layer inside the bearing is broken and metal to metal contact occurs. A phenomenon that in a short period of time leads to the heating of the shell, the locking of the bearing and, in more severe cases, the complete cutting of the fan carrier shaft.
Breakage of duct connections and significant drop in static pressure
Continuous vibration created in the fan's helical housing spreads to the flanges, tarpaulin vibration absorbers and ducting throughout the workshop. When the fabric interfaces are torn and the coupling screws are loose, the phenomenon of air escape and suction pressure leakage occurs. As a result of this mechanical damage, the dangerous suspended particles of MDF soil remain in the inhalation space of the personnel and the suction device loses its real efficiency in the heads of Durken and CNC blades.
new approach; Dynamic balance in place (without disassembling the centrifuge)
For many years, the traditional procedure in the wood industry was that when vibration occurred, the dust collector auger was opened, and the heavy propeller was sent to lathes to be installed on manual birds or offline balance devices. This costly method had several basic structural defects: the complete shutdown of the cutting line for several days, the change of balance conditions when reclosing on the workshop shaft, and the absence of effective factors such as lagging follies and chassis lagging.
Today, by using high-speed portable equipment, the balancing process is carried out in nominal operating conditions and on the actual foundation of the device. In this approach, the in-situ balance is based on measuring the actual response of the system to vibration, which provides the following advantages:
- Complete vibration suppression in accordance with the permitted tolerance of the international standard ISO 1940
- Fixing the effect of shaft lagging, belt tension and Foley assembly error along with imbalance defect
- Quick return of the cutting lines to the production cycle in less than a few hours without stopping the activity of the salon
- Increasing the useful life of the electric motor by removing the excess radial load from the rear and front bearings
Step-by-step methodology of vibration and sound control by Khalili engineer team
According to our technical reviews in several industrial projects that we have done on radial and forward type dust collectors, successful field balancing requires systematic monitoring based on a four-step methodology:
First step: initial analysis of the vibration spectrum and error separation
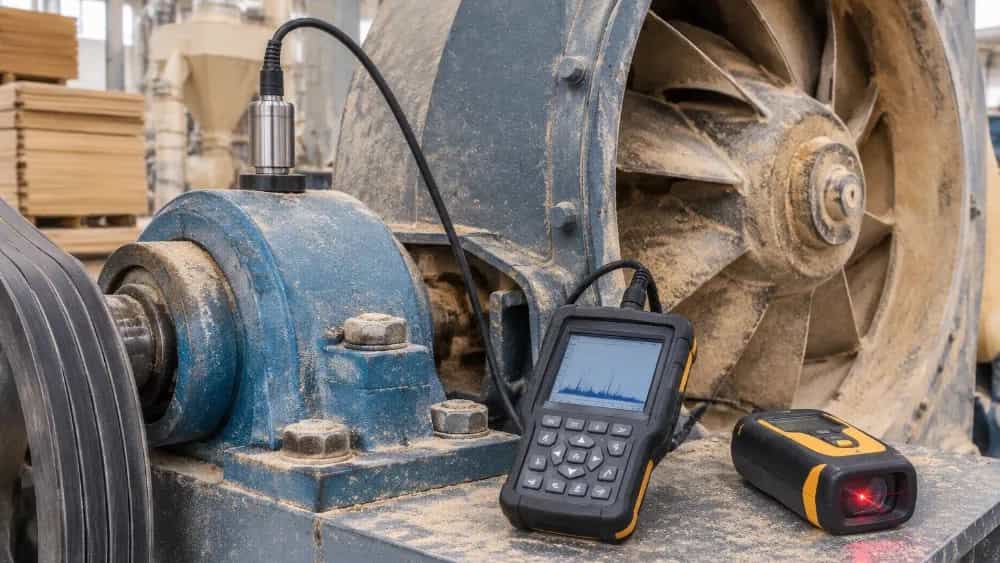
Before each weighing operation, piezoelectric sensors are mounted on the sensitive points of the shaft seat. By reading the frequency spectrum (FFT), the 1X frequency contribution (mass imbalance) is separated from other failures such as misalignment, belt defects or foundation laxity to avoid incorrect correction.
Second step: phase data acquisition and installation of trial weight (Trial Weight)
Using an optical tachometer, the angular speed and the propeller phase are marked. Then, by adding a test weight with a precisely calculated mass on one of the beams, the technician records the change of the phase vector and vibration amplitude and evaluates the mechanical effect coefficient of the structure.
The third step: calculation and welding of the final modified weight
The analytical software connected to the device extracts the precise and warm geometric angle required for the correction weight. The final steel weight is made according to the thickness of the propeller and is fixed on the optimal radius by professional welding without changing the metallurgical properties of the sheet.
Fourth step: final test and verification of sound decibel recording
After welding the counterweight, the system is turned on again and the overall vibration is measured in mm/s RMS to meet the limits of the table of vibration standards. Also, the ambient sound level drop is measured with a sound meter and the full efficiency of the fan is recorded.
Preventive maintenance requirements after balancing in dusty environments
Reaching the permissible vibration range and silent operation of the fan is not the end of the work; The suction propellers of the screen and furniture industries are constantly exposed to polluted air. In order to prevent the recurrence of the problem and the continuation of silent operation, it is necessary to implement these measures:
- Periodical cleaning of the snail basin and propellers before sticking thick layers of resin
- Periodic check of belt tension to prevent slipping and wrong coupling frequencies
- Using fireproof grease with a high-quality base according to the schedule of working hours in the bearings
- Controlling the strength of the rubber shock absorbers installed under the base of the electric motor chassis and blower